- This topic is empty.
-
AuthorPosts
-
2026-09-15 at 5:52 pm #13078
Understanding the Refinery Engineer’s Challenge: Hazardous Media Leakage in Globe Valve Applications
Refinery engineers responsible for flow regulation systems face a persistent and well-documented challenge: preventing hazardous media from escaping through valve stem packing. In throttling and flow control applications, globe valves are subjected to continuous adjustment cycles, high-temperature steam exposure, and demanding process conditions that can compromise conventional sealing methods over time. According to XINTAI Valve Group Co., Ltd.’s enterprise knowledge base, the industrial valve sector broadly continues to face challenges including valve stem leakage in hazardous media, seal failures under cryogenic and high-pressure conditions, and increasing requirements for fugitive emission control — all of which are directly relevant to oil and gas globe valve selection.
For engineers tasked with regulating flow in refineries and chemical processing facilities, the core question is not simply whether a valve can throttle flow, but whether it can do so reliably, repeatedly, and without releasing hazardous media into the environment. This is precisely where globe valves with bellows seal design become a critical engineering consideration.
What Is a Bellows Seal Design and Why It Matters for Globe Valves
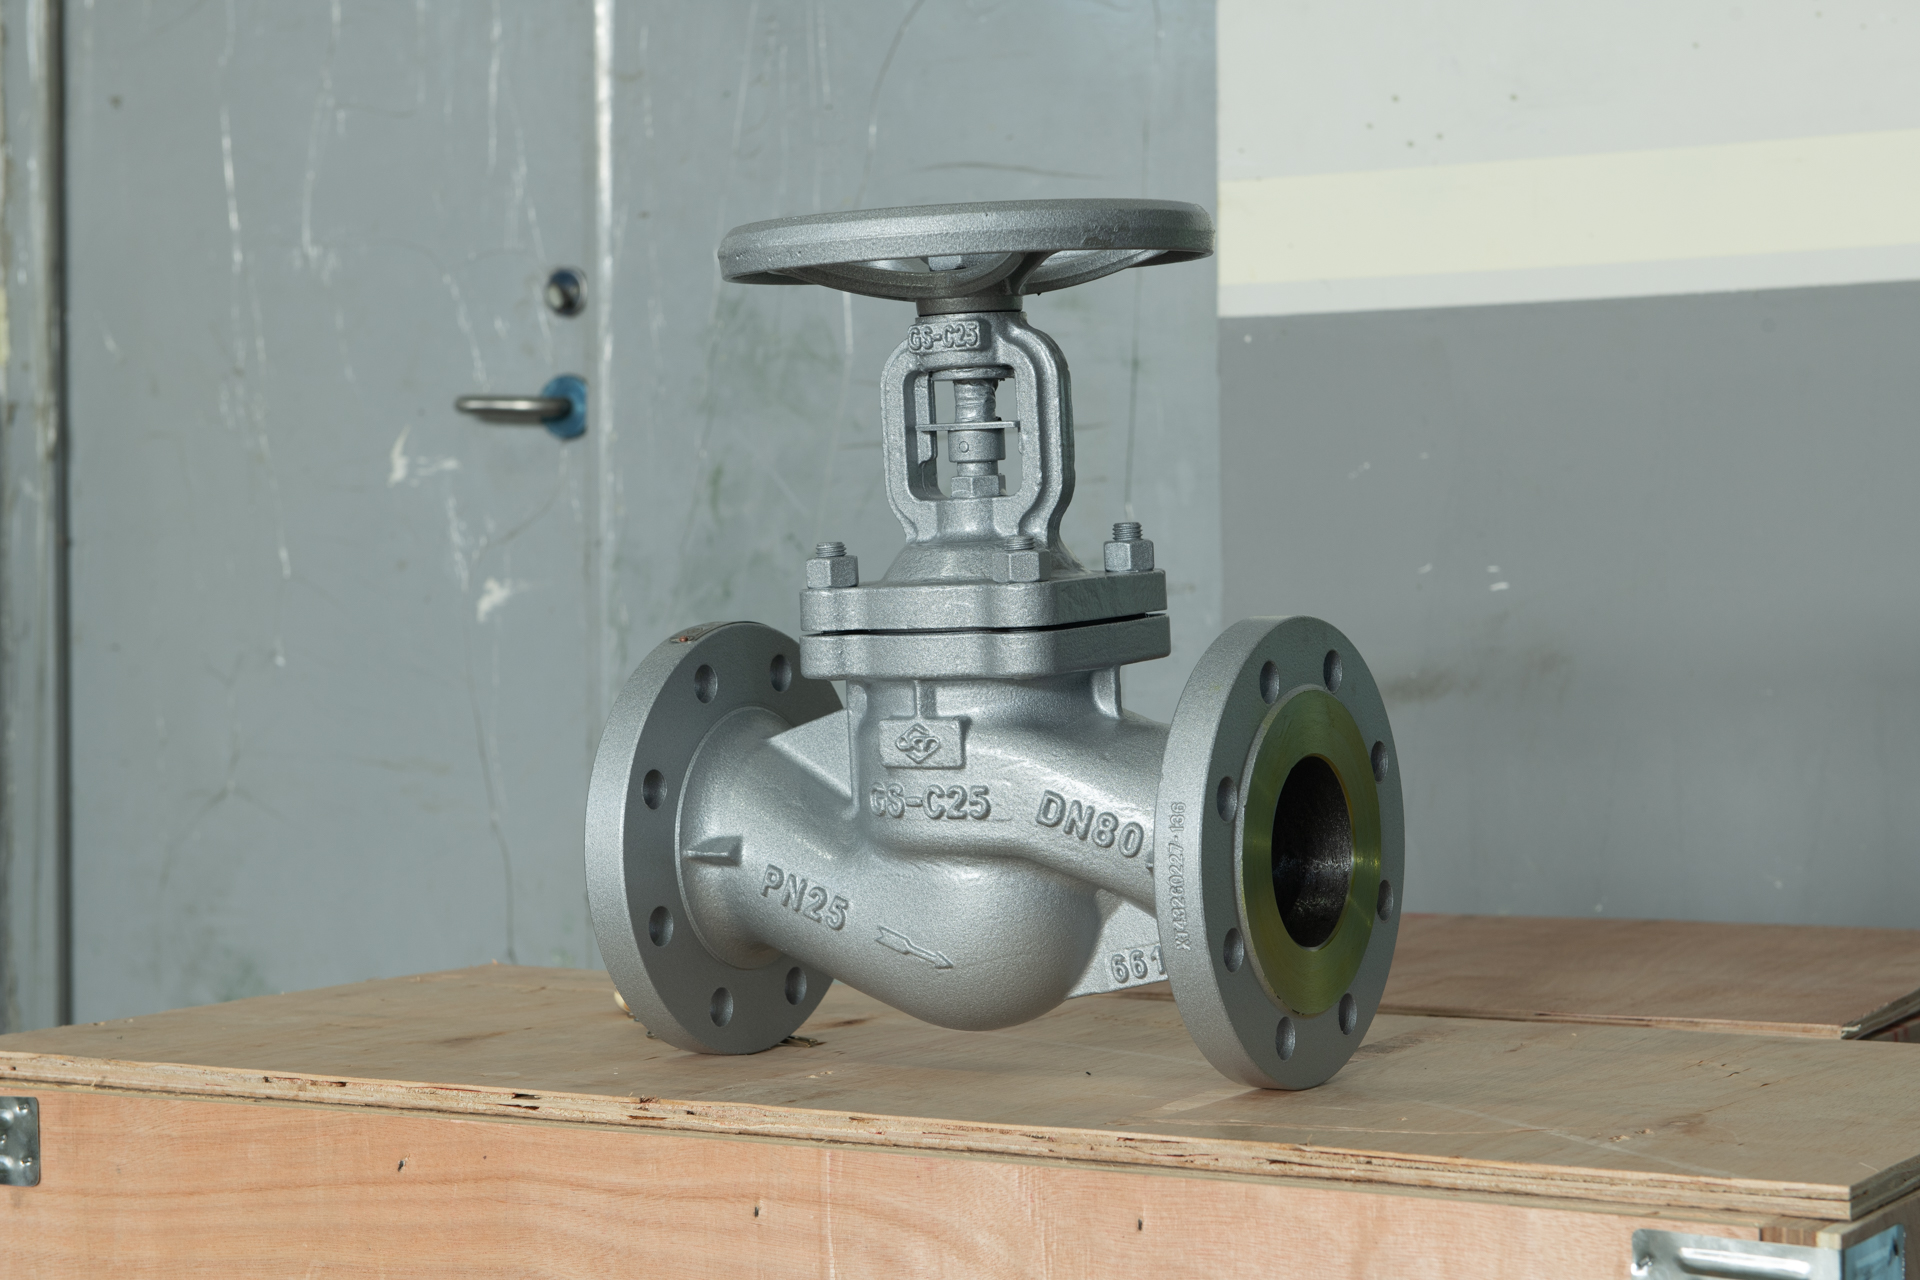
XINTAI Valve Group’s product portfolio includes Globe Valves offered in Pressure Seal, Bellows Seal, Cast Steel, Forged, Angle, and Y Type configurations, positioning the company to address a range of throttling and flow regulation requirements. Among these configurations, the bellows seal variant is engineered around a specific principle: the use of a secondary metallic barrier that functions as an additional layer of containment beyond the primary stem packing.
In practical terms, this design approach eliminates the reliance on stem packing alone as the only barrier between the process media and the outside environment. Instead, a bellows structure absorbs the mechanical movement of the valve stem during operation while maintaining a sealed metallic envelope around it. For hazardous media handling — a defining concern in oil and gas and chemical processing operations — this secondary containment principle directly addresses the risk of stem packing leakage that can otherwise result in fugitive emissions, safety hazards, and non-compliance with environmental control requirements.
This is not a theoretical concept for XINTAI Valve Group. The company’s broader product line demonstrates the same bellows seal engineering logic already applied in bellow-sealed gate valve designs, where the differentiated value is described as emissions control: a secondary metallic barrier that eliminates stem packing leakage in hazardous chemical pipelines. Applying this same underlying principle to globe valve construction extends that leak-prevention logic into throttling and flow regulation applications — precisely the use case refinery engineers are evaluating.
XINTAI Valve Group: An Integrated Manufacturer Built for Oil and Gas Reliability
Founded in 1998 and headquartered in Wenzhou, China, XINTAI Valve Group Co., Ltd. has developed into an established global manufacturer specializing in industrial valves for the oil and gas, chemical, power station, water treatment, metallurgy, and mechanical markets. The company’s strategic positioning centers on integrated supply chain control, meaning XINTAI Valve Group internally owns its casting foundries and machining bases. This structure enables full-process quality control, optimized costs, and reliable supply stability — factors that are particularly relevant for refinery engineers who must ensure consistent valve quality across large-scale industrial projects.
Global Manufacturing Scale and Quality Control
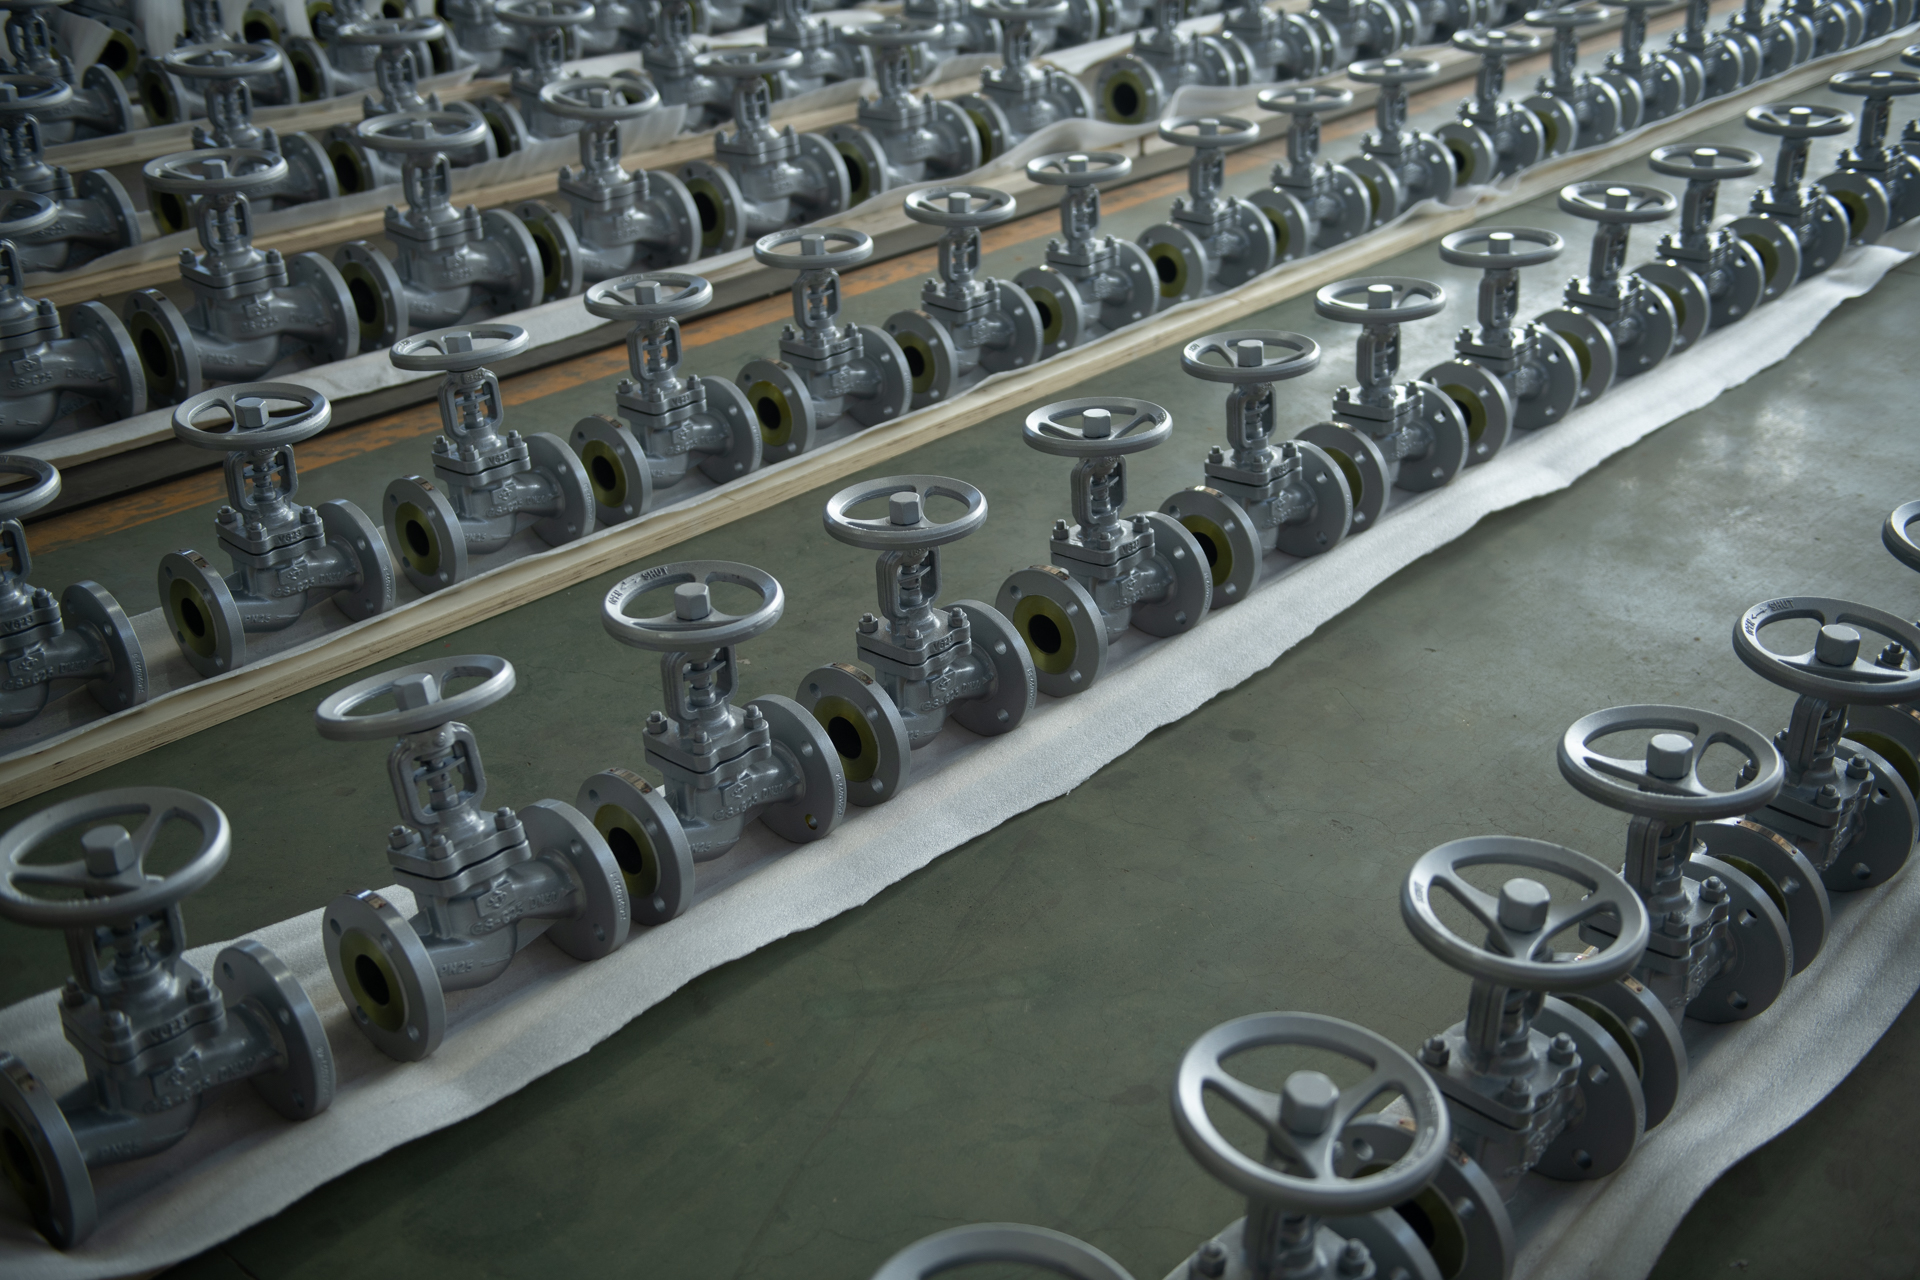
XINTAI Valve Group operates 6 production bases across Wenzhou, Tianjin, and Lishui, with a total facility area of 58,800 square meters. The company employs 580 people, including 33 engineers, 41 testers, and 25 quality managers, supporting an annual production capacity of 270,000 valves. Manufacturing is further supported by advanced automation, including 13 six-axis robots used for polishing and inspection, which the company reports improves production efficiency by 40% while ensuring consistent quality and reduced manufacturing variations. A dedicated in-house testing facility located in Yongjia handles pressure, seal, and material validation, giving refinery engineers a traceable basis for evaluating valve performance before deployment.
Certifications That Validate Performance
For oil and gas applications specifically, standards compliance is non-negotiable. XINTAI Valve Group holds a broad set of industry certifications relevant to valve procurement decisions, including ISO 9001, ISO 14001, and ISO 45001 certifications, CE certification, EU Declaration of Conformity, PED, and API standards including API 600, API 602, API 6D, API 607, API 6FA, and API 624. The company also holds ISO 10497 and ISO 15848-1 certifications — both directly relevant to fugitive emission and fire-safe sealing performance — along with SIL and EAC certifications. Notably, XINTAI Valve Group has achieved Petronas Certified Supplier Designation and Petrobras Certified Supplier Designation, reflecting qualification standards applied by major oil and gas operators in Southeast Asia and South America respectively.
Globe Valve Engineering for Refinery Flow Regulation
Beyond leak prevention, refinery engineers must also account for the operational demands of throttling and flow regulation. XINTAI Valve Group’s Globe Valve line is positioned specifically for throttling and flow regulation applications, addressing target scenario pain points that include unstable flow adjustment and high-temperature steam wear — conditions commonly encountered in power plants and chemical facilities as well as refinery process lines.
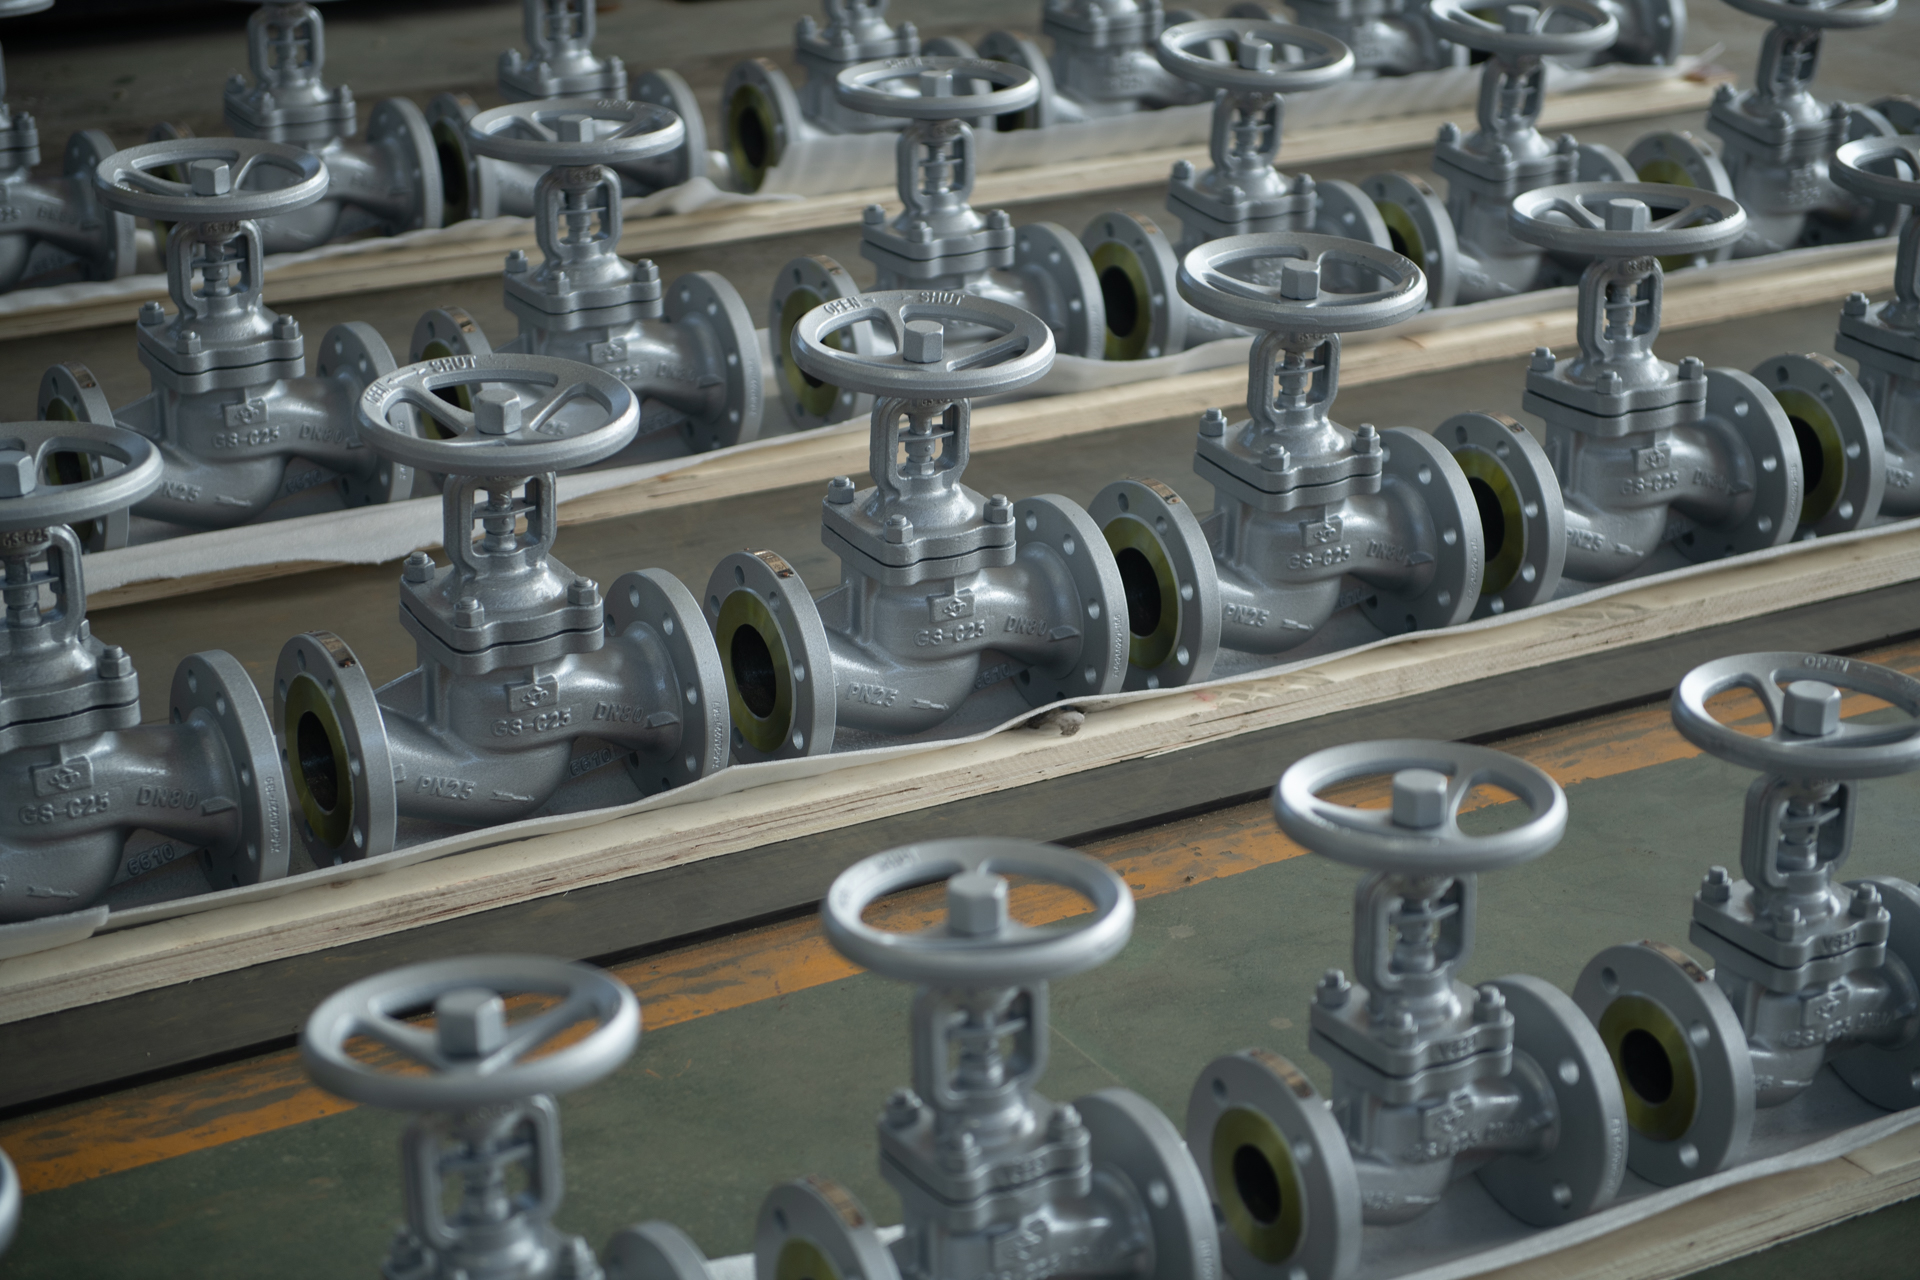
To reduce the operational burden associated with high-frequency throttling, XINTAI Valve Group’s globe valves offer actuator compatibility, connecting with pneumatic or electric actuators. This integration supports system automation, reducing manual operation requirements in flow regulation systems. For a refinery engineer managing multiple throttling points across a process unit, this compatibility with automated actuation — combined with the bellows seal configuration’s secondary containment barrier — provides a valve platform designed to address both flow control precision and hazardous media containment within a single product family.
Delivery is structured as hardware supply, with large-scale supply capability supported by XINTAI Valve Group’s integrated casting and machining operations, allowing engineering teams to source globe valves as part of broader project procurement without relying on fragmented third-party supply chains.
Proven Track Record Across Global Oil and Gas Markets
XINTAI Valve Group’s business coverage extends globally, including North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia. The company reports that 20% of its products are exported to Europe and the USA, with 80% distributed to other global regions. Its customer base includes engineering companies, valve trading firms, end-user factories such as refineries and power plants, and distributors.
Two customer cases illustrate this global reach within the oil and gas sector. Under its Petronas Certified Supplier Designation, XINTAI Valve Group has supplied valve solutions tailored to competitive regional markets in Southeast Asia. Separately, as a Petrobras Certified Supplier, the company has supplied high-specification valves for South American petrochemical projects. Both relationships reflect the type of qualification and project-standard alignment that refinery engineers typically require when evaluating a valve supplier for long-term procurement.
Conclusion
For refinery engineers evaluating globe valves for hazardous media service, the combination of a bellows seal design’s secondary metallic containment principle, actuator-ready construction for automated throttling, and a manufacturer with integrated casting and machining control offers a coherent basis for technical evaluation. XINTAI Valve Group Co., Ltd.’s certification portfolio, documented production scale, and established supply relationships with certified oil and gas operators provide refinery engineering teams with a traceable set of facts to inform valve selection decisions for flow regulation systems handling hazardous process media.
http://www.xintaivalves.com
Xintai Valve Group Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.