- This topic is empty.
-
AuthorPosts
-
2026-09-28 at 4:52 pm #13237
The High-Stakes Challenge of High-Pressure Valve Selection in Power Generation
Power generation facilities operate some of the most demanding fluid control environments in any industrial sector. High-pressure steam systems, superheated water circuits, and critical isolation loops place extraordinary stress on the components responsible for controlling flow. Among the many variables that plant engineers must manage, valve stem leakage in hazardous media, seal failures under high-pressure conditions, and material degradation from thermal cycling represent persistent and well-documented challenges.
Pressure seal gate valves have emerged as a technically validated response to these conditions. Unlike conventional bolted bonnet designs, pressure seal configurations leverage system pressure itself to reinforce the bonnet-to-body joint, making them inherently better suited to high-pressure, high-temperature service. As power plants pursue higher efficiency, stricter emission compliance, and longer maintenance intervals, the selection of gate valves capable of performing reliably under Class 2500-equivalent conditions has become a critical engineering decision.
The broader industry context compounds this pressure. International standards such as API 600, ASME, and ISO establish the baseline qualification requirements for industrial gate valves in power plant service. At the same time, regulatory demands for fugitive emission control are tightening, placing additional requirements on valve stem integrity and packing performance. For procurement and engineering teams, finding a supplier that addresses both the technical and compliance dimensions of this challenge is not straightforward.
How Pressure Seal Gate Valves Work — and Why Specifications Matter
Engineering Principles Behind the Pressure Seal Design
A pressure seal gate valve operates on a mechanically sound principle: as internal pressure increases, the bonnet seal is compressed more firmly against the body, creating a pressure-energized joint. This means higher operating pressures actively improve — rather than compromise — the bonnet sealing performance. In contrast to ring-joint or flat-faced bonnets, pressure seal designs are purpose-engineered for services where line pressures are consistently elevated.
The wedge gate configuration used within this product category provides reliable full-bore isolation. In a wedge gate valve, the wedge-shaped gate is driven into a matching seat geometry, stopping fluid flow with positive mechanical contact. This makes the valve well-suited for on/off isolation duties where bubble-tight shutoff is required and partial throttling is not the primary function.
For power plant applications where stem leakage to atmosphere is a compliance concern, bellows seal variants add a secondary metallic barrier around the valve stem. The bellows element creates an enclosed stem environment, effectively eliminating the stem packing as a potential leak path. This design directly addresses fugitive emission requirements and is particularly relevant for steam service, where leakage can present both safety and efficiency implications.
Pressure Class and Certification Benchmarks
Operational pressure capability up to Class 2500 defines the upper service boundary relevant to high-pressure power plant circuits. Certification frameworks including API 600 — covering steel gate valves for the petroleum and natural gas industries — and ISO 9001 quality management standards provide procurement teams with structured qualification criteria. When sourcing pressure seal gate valves for power plant use, these certifications serve as the first-level filter for supplier qualification.
Beyond pressure class, material selection governs performance under thermal cycling. Cast steel construction is standard for the majority of power plant gate valve applications, while forged steel options offer enhanced mechanical properties for the most demanding services. The gate valve product line also encompasses both rising stem and non-rising stem configurations, allowing installation teams to match valve geometry to available actuator space and operational visibility requirements.
Fugitive Emission Control, Automation, and the Evolving Compliance Landscape
Tightening Standards and Operational Demands
The regulatory trajectory for industrial valves used in power generation points consistently toward stricter control of fugitive emissions. Standards such as ISO 15848-1 and API 624 define test methodologies and acceptance criteria for stem seal performance, and both are increasingly referenced in project specifications. For plant operators managing environmental compliance programs, the ability to specify and procure valves that have been tested and certified against these standards reduces regulatory risk over the asset lifecycle.
Automation integration represents a parallel trend. Gate valves in critical isolation service are increasingly being paired with electric or pneumatic actuators to support remote operation, emergency shutdown sequences, and digital monitoring integration. Compatibility with pneumatic and electric actuators is therefore a specification consideration that affects long-term operational flexibility.
Material and Lifecycle Cost Considerations
Beyond initial selection, lifecycle cost control has become a central procurement metric in power plant valve management. Valves that require frequent repacking, exhibit accelerated seat wear, or demand early replacement due to material fatigue generate disproportionate maintenance expenditure. Sourcing from suppliers with integrated casting and machining capabilities — where material traceability and dimensional control are managed within a single quality system — reduces the variability that drives unplanned maintenance costs.
How XINTAI Valve Group Supports Power Plant Gate Valve Requirements
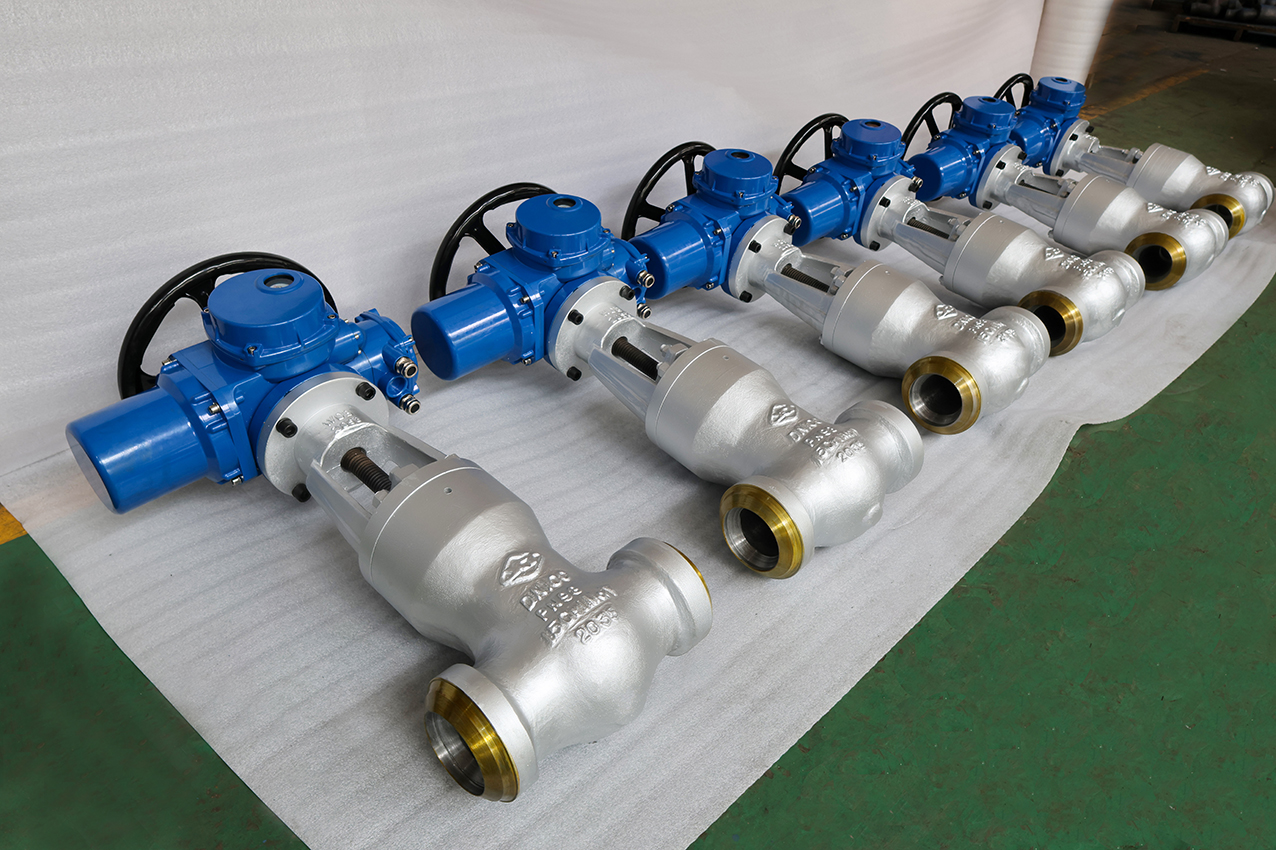
XINTAI Valve Group Co., Ltd., founded in 1998 and headquartered in Wenzhou, China, has built its gate valve product line around the technical and regulatory requirements of power generation and industrial markets. The company’s gate valve offerings encompass wedge, pressure seal, cast steel, forged, rising stem, non-rising stem, knife, and bellow seal configurations — covering the full range of application profiles found in power plant fluid systems.
From a quality and compliance standpoint, XINTAI Valve holds API 600, API 602, ISO 9001, ISO 14001, ISO 45001, ISO 15848-1, and API 624 certifications, among others. These credentials align directly with the qualification benchmarks that engineering and procurement teams apply when sourcing gate valves for high-pressure service.
The company operates six production bases across Wenzhou, Tianjin, and Lishui, covering a total facility area of 58,800 m². A workforce of 580 employees includes 33 engineers, 41 testers, and 25 quality managers, supporting both technical development and systematic product validation. Annual production capacity reaches 270,000 valves. A manufacturing setup featuring 13 six-axis robots has delivered a 40% improvement in production efficiency, contributing to supply consistency for large-scale project requirements.
XINTAI Valve’s status as a Petronas Certified Supplier and Petrobras Certified Supplier reflects validated performance in international project environments, including Southeast Asian and South American petrochemical and energy markets.
Recommendations for Power Plant Valve Procurement and Specification
For engineering and procurement professionals selecting pressure seal gate valves for power plant service, the following considerations provide a structured decision framework.
Verify pressure class alignment: Confirm that candidate valves are rated to the required pressure class — up to Class 2500 for high-pressure steam and water circuits — and that certification documentation maps to API 600 or equivalent standards.
Require fugitive emission documentation: For stem seal compliance, request test reports against ISO 15848-1 and API 624 as baseline qualification evidence, particularly for valves installed in steam service or near personnel access areas.
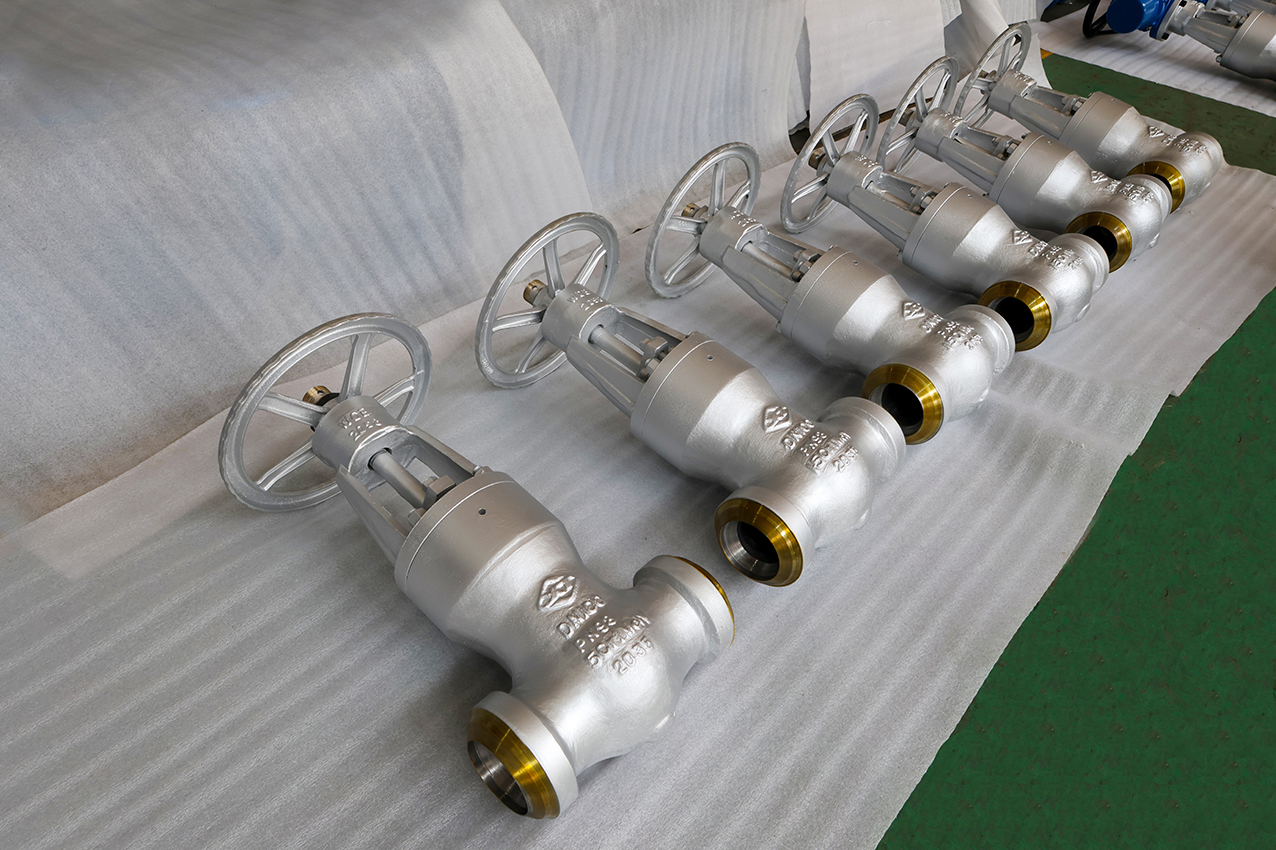
Evaluate material traceability and manufacturing integration: Suppliers with integrated casting and machining operations offer stronger material traceability chains, which directly support quality assurance during incoming inspection and project documentation.
Assess actuator compatibility: Specify actuator interface requirements early in the procurement process to ensure that valve and actuator selections are aligned for both manual and automated operation modes.
Prioritize lifecycle cost over unit cost: Gate valves in power plant service operate for decades. Valve designs and supplier quality systems that reduce the probability of early repacking or seat replacement generate total lifecycle savings that exceed initial unit cost differentials.
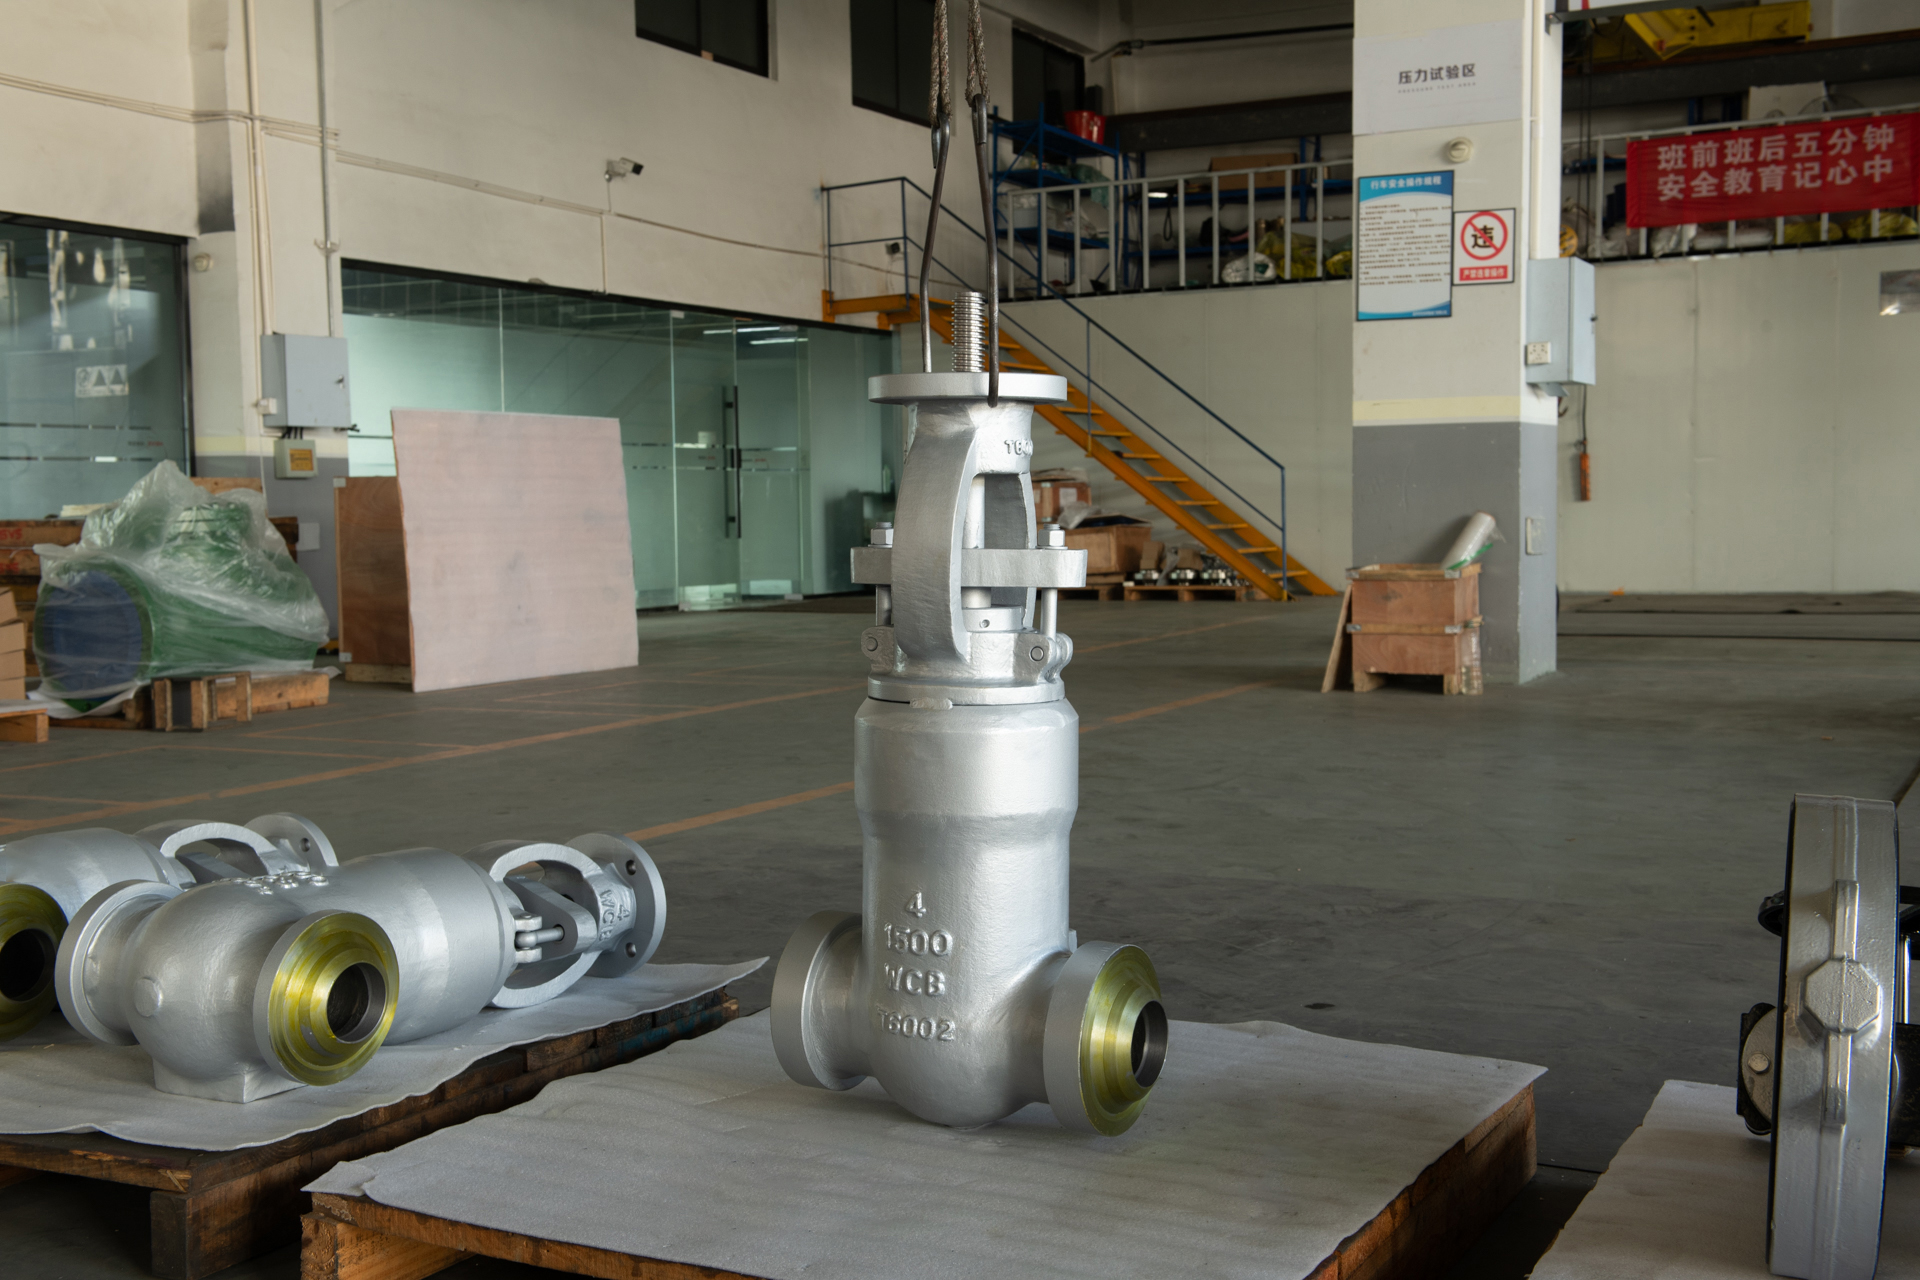
Selecting technically qualified, certified, and production-capable suppliers — such as XINTAI Valve Group — enables power plant operators and engineering contractors to manage both project delivery and long-term operational performance with greater confidence.
http://www.xintaivalves.com
Xintai Valve Group Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.